
Top 7 Common 3D Printing Problems and How to Fix Them Like a Pro
3D printing opens a world of creative possibilities, from crafting custom designs to prototyping functional parts. However, even with the advanced technology of 2025, beginners often encounter frustrating issues that can derail their projects. Don’t worry! This guide covers the top 7 common 3D printing problems and provides pro-level solutions to get your prints back on track. Whether you’re using an FDM or resin printer, these tips will help you troubleshoot like a seasoned maker. Ready to master your 3D printing journey? Let’s dive in!
Struggling with 3D printing issues? This guide will help you fix them like a pro!
Why 3D Printing Problems Happen
Even the best 3D printers, like those recommended on our homepage, can face challenges due to misaligned settings, environmental factors, or user error. Understanding these issues is the first step to fixing them. Most problems are easy to resolve with the right knowledge, saving you time and filament. Let’s explore the most common issues and how to tackle them like a pro.
1. Poor Bed Adhesion (Prints Not Sticking)
Problem: Your print lifts off the bed, warps at the edges, or detaches completely, ruining the model.
Why It Happens: Poor bed adhesion occurs when the first layer doesn’t bond properly to the print bed, often due to an uneven bed, incorrect settings, or a dirty surface.
How to Fix It Like a Pro:
- Clean the Bed: Wipe the print bed with isopropyl alcohol (70–90%) and a lint-free cloth to remove dust, oils, or residue.
- Level the Bed: Use auto bed leveling (available on printers like the Bambu Lab A1 from our homepage) or manually adjust the bed to ensure it’s perfectly flat.
- Adjust First Layer Settings: Increase bed temperature (e.g., 60°C for PLA) and slow the first layer speed to 20–30 mm/s in your slicer (e.g., Cura).
- Use Adhesives: Apply a thin layer of glue stick, painter’s tape, or hairspray to improve grip.
- Check Nozzle Height: Ensure the nozzle is close enough to the bed (about the thickness of a piece of paper) for a strong first layer.
Pro Tip: Print a test model like 3DBenchy to check adhesion before starting complex projects.
2. Stringing (Wispy Strands on Prints)
Problem: Thin, stringy filaments appear between parts of your print, creating a messy, cobweb-like effect.
Why It Happens: Stringing occurs when melted filament oozes from the nozzle during non-printing movements, often due to improper retraction settings or high temperatures.
How to Fix It Like a Pro:
- Adjust Retraction Settings: In your slicer, increase retraction distance (2–5 mm for PLA) and speed (40–60 mm/s) to pull filament back when moving.
- Lower Print Temperature: Reduce nozzle temperature by 5–10°C (e.g., 200°C for PLA) to minimize oozing.
- Enable Combing: Turn on combing in your slicer to keep the nozzle within the print area, reducing unnecessary travel.
- Dry Filament: Wet filament can cause stringing. Store filament in a dry box or dry it in an oven at 45°C for 4–6 hours.
Pro Tip: Run a retraction test print (available on sites like Printables) to fine-tune settings.
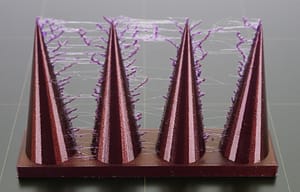
Stringing can ruin a print, but simple tweaks can fix it.
3. Layer Shifting or Misalignment
Problem: Layers of your print shift, creating a skewed or stepped appearance.
Why It Happens: Layer shifting is caused by mechanical issues (loose belts or pulleys), excessive print speed, or collisions between the nozzle and the print.
How to Fix It Like a Pro:
- Check Belts and Pulleys: Tighten belts and ensure pulleys are secure. Use a screwdriver to check for loose screws on your printer (e.g., Creality Ender-3 V3 SE from our homepage).
- Reduce Print Speed: Lower speed to 50–80 mm/s in your slicer to prevent vibrations.
- Ensure Proper Cooling: Add a cooling fan or increase fan speed to solidify layers before the next pass.
- Clear Obstructions: Ensure the print head moves freely and the bed is stable.
Pro Tip: Lubricate rails with silicone-based lubricant to improve smooth movement.
4. Warping (Corners Lifting)
Problem: The edges or corners of your print curl upward, distorting the model.
Why It Happens: Warping occurs when filament cools unevenly, causing contraction. This is common with materials like ABS or large prints.
How to Fix It Like a Pro:
- Increase Bed Temperature: Use 60–70°C for PLA or 90–100°C for ABS to maintain consistent heat.
- Use an Enclosure: Enclosed printers (like the Anycubic Kobra 2 Plus from our homepage) reduce drafts and maintain stable temperatures.
- Add a Brim or Raft: In your slicer, add a brim (8–10 mm) or raft to increase bed adhesion and stabilize the print.
- Control Room Temperature: Keep your printing area at 20–25°C and avoid open windows or fans.
Pro Tip: Apply a thin layer of glue stick to the bed for extra adhesion on large prints.
5. Under-Extrusion (Gaps or Weak Prints)
Problem: Your print has gaps, thin layers, or missing sections due to insufficient filament extrusion.
Why It Happens: Under-extrusion can result from clogged nozzles, incorrect filament settings, or low-quality filament.
How to Fix It Like a Pro:
- Clean the Nozzle: Perform a cold pull or use a cleaning filament to clear blockages. Heat the nozzle to 220°C (for PLA) and push filament through manually.
- Check Filament Diameter: Ensure your slicer matches the filament diameter (usually 1.75 mm).
- Adjust Flow Rate: Increase flow rate by 5–10% in your slicer to compensate for under-extrusion.
- Use Quality Filament: Opt for trusted brands like Hatchbox or eSun (available via our homepage) to avoid inconsistent filament.
Pro Tip: Replace worn nozzles (0.4 mm is standard) every 3–6 months for consistent extrusion.
6. Over-Extrusion (Blobby or Bulging Prints)
Problem: Excess filament creates rough, bulging, or overly thick layers, ruining print quality.
Why It Happens: Over-extrusion occurs when too much filament is extruded, often due to incorrect flow settings or high temperatures.
How to Fix It Like a Pro:
- Reduce Flow Rate: Decrease flow rate by 5–10% in your slicer (e.g., set to 90–95%).
- Lower Temperature: Reduce nozzle temperature by 5–10°C to prevent excessive melting.
- Calibrate E-Steps: Adjust extruder steps per mm (check your printer’s manual for instructions) to ensure accurate filament feeding.
- Inspect Filament: Ensure consistent filament diameter to avoid overfeeding.
Pro Tip: Print a calibration cube to test extrusion accuracy and fine-tune settings.
7. Failed Prints (Print Stops Mid-Process)
Problem: Your print stops unexpectedly, leaving an incomplete model.
Why It Happens: Failed prints can stem from power issues, filament jams, software glitches, or overheating components.
How to Fix It Like a Pro:
- Check Filament Supply: Ensure filament isn’t tangled or running out. Use a filament runout sensor if available.
- Verify Power Stability: Use a UPS (uninterruptible power supply) to prevent power interruptions.
- Update Firmware: Ensure your printer’s firmware is up-to-date (check manufacturer’s website).
- Monitor Temperatures: Prevent overheating by ensuring proper cooling for the printer’s electronics.
Pro Tip: Enable “resume on power loss” in your printer’s settings (if supported) to recover from interruptions.
Quick Reference: Common 3D Printing Problems and Fixes
| Problem | Likely Cause | Quick Fix |
|---|---|---|
| Poor Bed Adhesion | Dirty or uneven bed | Clean bed, level bed, use adhesive |
| Stringing | Improper retraction | Adjust retraction, lower temperature |
| Layer Shifting | Loose belts, high speed | Tighten belts, reduce speed |
| Warping | Uneven cooling | Use enclosure, add brim/raft |
| Under-Extrusion | Clogged nozzle, low flow | Clean nozzle, adjust flow rate |
| Over-Extrusion | High flow, high temperature | Reduce flow, lower temperature |
| Failed Prints | Filament or power issues | Check filament, use UPS, update firmware |
Tips to Prevent 3D Printing Problems
- Start with Quality Equipment: Choose reliable printers like those on our homepage to minimize issues.
- Use Trusted Filament: Brands like Hatchbox or eSun ensure consistent quality.
- Calibrate Regularly: Check bed leveling and extruder settings before major prints.
- Join Communities: Reddit’s r/3Dprinting or brand-specific forums offer troubleshooting advice.
- Test Small Prints: Use small test models (e.g., 3DBenchy) to dial in settings before large projects.
- Maintain Your Printer: Clean the bed, lubricate rails, and check for loose screws monthly.
How to Get Started with Confidence
To avoid these issues from the start:
- Choose the Right Printer: Visit our homepage for beginner-friendly recommendations like the Bambu Lab A1 or Creality Ender-3 V3 SE.
- Learn Your Slicer: Master Cura or PrusaSlicer with online tutorials to optimize settings.
- Start Simple: Download free models from Thingiverse or Printables to practice.
- Document Settings: Keep a log of successful print settings for each filament type.
Conclusion
3D printing problems are part of the learning curve, but with these pro-level fixes, you can troubleshoot like a seasoned maker. From bed adhesion to failed prints, the solutions above will keep your projects on track. Invest in a reliable printer from our homepage, practice with small models, and join the 3D printing community to refine your skills. Soon, you’ll be printing flawless models with confidence!
Got a 3D printing issue? Share it in the comments, and let’s troubleshoot together!